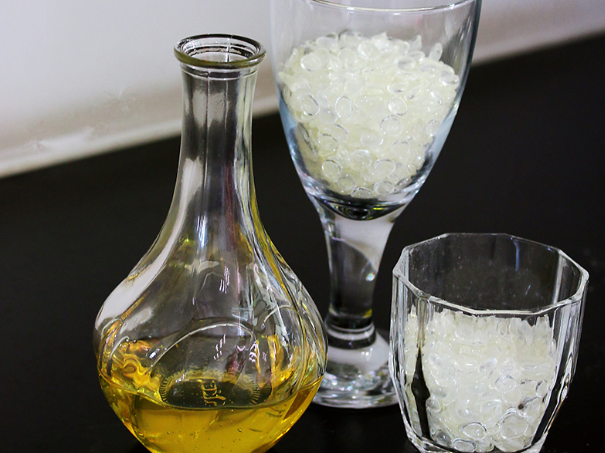
Data-driven introduction to process limits
Manufacturing robust adhesive lines requires quantifiable limits on how much a rosin tackifier’s softening point can shift during processing. Recent line audits show that small shifts in softening point correlate strongly with end-use tack and set time, so formulators now use instrumented sampling and batch-level control. Early in the run, blend trials with tackifying resin establish a baseline softening point and viscosity target; these baselines are then treated as control limits across downstream mixing and melt transfer operations.
Why softening point shifts matter for heavy-duty lines
Softening point directly influences adhesive film flow, hot-melt pot life, and grab performance on difficult substrates. For bulk rosin tackifiers, a downward drift can mean longer open time but weaker green strength; an upward drift tightens spread but risks poor wetting. Quantitatively, manufacturing teams track softening point as a sentinel variable because it integrates effects from acid number, molecular weight distribution, and thermal history—three variables that dictate viscosity and adhesion on coated lines.
Interpreting ASTM E28 constraints in production
ASTM E28-20, “Standard Test Method for Softening Point of Resin—Ring-and-Ball Apparatus,” provides the test framework production labs must follow. Relevant sub-sections include “Apparatus” (which describes ring dimensions and ball materials), “Sampling” (sample mass and conditioning), and “Procedure” (which specifies a controlled heating rate of 5 °C per minute and timing for ball placement). Operations teams adapt these clauses to quality control by running the exact “Procedure” parameters for every lot to avoid method bias when comparing batches.
Operational production teardown: what to measure and where
A practical teardown breaks the line into feed, melt, hold, and transfer stages and attaches metrics to each. Measure inlet resin temperature, hold-tank residence time, shear exposure in the pump, and final pot temperature. Track softening point and viscosity at three control points: post-melt, post-hold, and after filter housings. In the operational production teardown, {main_keyword} and {variation_keyword} provide naming for data tags and comparisons across shifts—this keeps feedback loops short. Pay attention to particle carryover at filters; small solids change heat transfer and will nudge softening point downward over several lots—address the root cause promptly.
Common mistakes and corrective tactics
Operators commonly assume single-point temperature control is sufficient; it is not. Thermal gradients in large tanks create pockets of overcooking that raise the apparent softening point for a slim fraction of the batch. The pragmatic fix is zone control and scheduled agitation cycles that reduce local overheating. Another frequent error is ignoring moisture pickup during transfer—moisture reduces effective resin concentration and can depress softening point. Correct by installing low-dead-volume transfer lines and inline dehydration where possible. Small investments in instrumentation yield outsized consistency gains.
Choosing and validating tackifier solutions
Select tackifier glue grades by their process robustness: low sensitivity to 1) thermal hold, 2) shear, and 3) minor oxidation. Validate candidates with a controlled stress test that repeats ASTM E28-20 “Procedure” after a simulated 8-hour hold at pot temperature, then again after a spray-dry exposure cycle. Compare softening point shifts and record viscosity recovery. Use these data to rank candidates and select the grade that stays within your allowable shift window—this is where formulation and line engineering converge.
Three golden rules for line designers
1) Set an operational softening point control band based on end-use performance, not just lab values—measure in-process and enforce limits. 2) Design thermal systems to keep residence time consistent; control heating to ±3 °C across zones and verify with thermocouple mapping. 3) Validate candidate resins under the ASTM E28-20 “Procedure” plus an extended-hold test; choose the grade with the smallest shift in softening point and stable viscosity under shear.
These rules lead to fewer rejects, predictable set times, and scalable batches—practical outcomes any production manager will value. For line-level solutions and validated grades that meet this operational logic, consider the product focus and application support offered by KOMO. —