Opening diagnosis — why choices go sideways
I write as someone used to standing on concrete shop floors and poring over layout prints; the problem-driven point here is simple — wrong choices early on cost time, money and safety. When engineers or procurement teams rush toward the fanciest specs or the lowest tender, they often miss crucial fit-for-purpose details. If you’re vetting prismatic battery pack assembly line suppliers, treat the first stage as a clinical assessment, not a shopping spree.

Mistake 1: Prioritising headline throughput without matching cycle reality
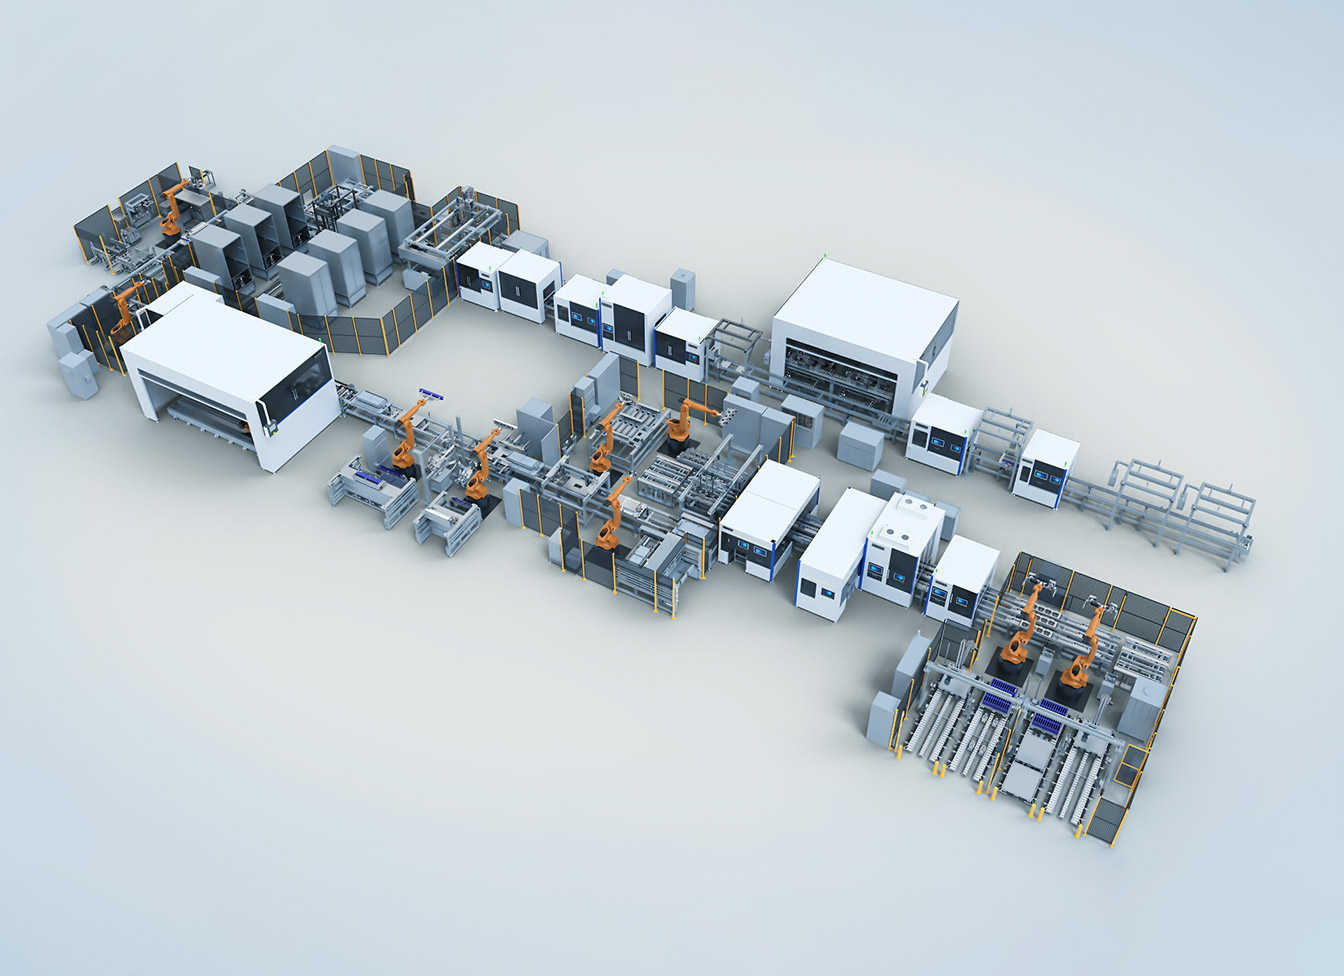
Teams take quoted max cycles at face value. That’s a mistake. Real-world throughput depends on cell handling, drying or curing steps, test time and unavoidable changeover. Avoidance steps:- Map your actual process steps and measure realistic cycle times.- Demand supplier evidence: factory acceptance test (FAT) scenarios that mirror your product mix.- Design for peak and modal throughput — not just the absolute maximum the vendor claims.
Mistake 2: Ignoring chemistry and form-factor nuances
Prismatic cells vary in thickness, terminal type and thermal behaviour. Selecting a line optimised for one cell variant and forcing another into it invites scrap and rework. Practical actions:- List every cell variant you currently run and might run within three years.- Require modular tooling and easy interchange procedures.- Verify sensor and handling settings are accessible for field adjustment.
Mistake 3: Treating integration as an afterthought
Robots, conveyors, testers, fume extraction and the MES all must speak the same language. Buyers who assume a supplier will “handle integration” without specific deliverables discover hidden costs. Mitigation:- Specify communication protocols, data formats and control handoffs up front.- Insist on documented I/O matrices and example OPC-UA endpoints.- Plan a short pilot run with live MES connectivity.
Mistake 4: Overlooking quality systems, standards and safety
Assembly lines must support inspection points, traceability and safety interlocks. Too many teams take a line and bolt processes on later. Best practice:- Require traceability to cell and module level as native functionality.- Confirm compliance with recognised standards such as IEC 62133 for cell safety and ISO 9001 for quality processes.- Check that emergency stops, light curtains and access interlocks meet local regulatory needs.
Mistake 5: Underestimating maintenance and spares planning
A sophisticated line is great until a critical fixture fails and production halts. Common fixes:- Ask suppliers for a recommended spares kit and lead times for wear parts.- Negotiate a service-level agreement with guaranteed response bands and remote diagnostic access.- Train local maintenance staff during FAT; don’t rely solely on remote support.
Mistake 6: Choosing rigidity over flexibility
Some lines perform brilliantly for a single SKU yet choke when demand shifts. Avoid permanent decisions that prevent future product changes:- Prefer modular stations that can be swapped or upgraded without a full rebuild.- Embed changeover time limits in contract performance metrics.- Keep mechanical drawings and PLC logic versioned and accessible.
Mistake 7: Skipping a realistic validation plan
Acceptance must reflect real product conditions. Too often acceptance tests are sterile and fail to catch thermal or mechanical edge cases. Build a validation plan that:- Includes environmental, vibration and electrical tests relevant to your application.- Uses statistical sampling for quality assurance rather than single-piece tests.- Allocates time for iterative fixes discovered during pilot runs.
Checklist for a problem-driven procurement
Use this compact checklist before signing:- Confirm supplier can run at least two of your SKUs in a FAT with production-speed cycles.- Obtain documented traceability and MES integration specifics.- Secure a spares list and guaranteed service response.- Lock in changeover times, modularity requirements and update access to PLC/HMI code.- Validate compliance with IEC 62133 and local electrical/safety requirements.
Where to inspect and what to look for
Visit a working facility when you can — many clients travel to Shenzhen manufacturing hubs to observe lines under load. At the visit watch for handling finesse, cell orientation guards, clear operator procedures and the presence of proper fume and ESD controls. Ask for time-stamped run data to confirm stability over several hours.
Quick decision framework
When comparing offers, score each on three axes and use the totals to decide:- Production fidelity: Can the supplier prove performance with your products?- Maintainability: Are spares, documentation and training included?- Compliance & safety: Does the line meet necessary standards and local codes?Weight production fidelity highest, but don’t let it eclipse maintainability and safety.
Closing synthesis
Do the diagnostic work, demand demonstrable proof and insist on modular, maintainable solutions; that approach reduces surprises and keeps costs under control. Practical experience shows that suppliers who can demonstrate real SKU runs, provide thorough documentation and commit to service response are the ones worth the partnership — which is precisely the grounded capability I’ve seen repeatedly from prismatic battery pack assembly line providers. For a selection process driven by problems, not promises, the right partner will help your team ship reliably, and often those reliable partners can be found through established integrators such as FHS.